
Views: 0 Author: Site Editor Publish Time: 2026-10-06 Origin: Site


Resin Transfer Molding (RTM) produces high-strength components. They boast precise, two-sided finishes. But this precision faces immediate jeopardy. The moment a part leaves the manufacturing floor, risks multiply. Standard shipping protocols frequently fail composite materials. They cause surface abrasions, edge chipping, or severe stress fractures. These failures destroy value instantly.
For procurement and engineering teams, evaluating a packaging protocol matters immensely. It proves just as critical as evaluating the manufacturing process itself. We must protect our composite investments from transit hazards. This guide breaks down the specialized packaging required. We explore methods to protect your components during transit and storage. You will learn how to match packaging designs to part geometries. We also reveal how to audit your vendor's logistics capabilities effectively. By understanding these logistics, you avoid costly reworks and production delays.
Generic packaging solutions fail rigid composite structures routinely. Many companies attempt to ship complex geometric parts using standard corrugated boxes. They place these boxes on generic wooden pallets. This approach ignores the fundamental material properties of composites. RTM parts possess high tensile strength but remain brittle against concentrated point-loads. Standard boxes offer zero structural support against these impacts.
Improper weight distribution creates invisible damage. When a pallet shifts during transit, unsecured parts collide. This transfers kinetic energy directly into the resin matrix. The impact causes microscopic fractures beneath the gel coat. These fractures remain invisible during standard receiving inspections. However, they expand under operational stress. This leads to catastrophic field failures long after delivery.
Inadequate packaging inflicts severe financial impacts across your organization. You must account for several distinct loss categories:
A successful packaging strategy prevents these issues entirely. It achieves a zero-defect arrival rate. Simultaneously, it maintains an efficient dimensional weight for freight calculations. You must balance maximum physical protection with minimum spatial footprint.
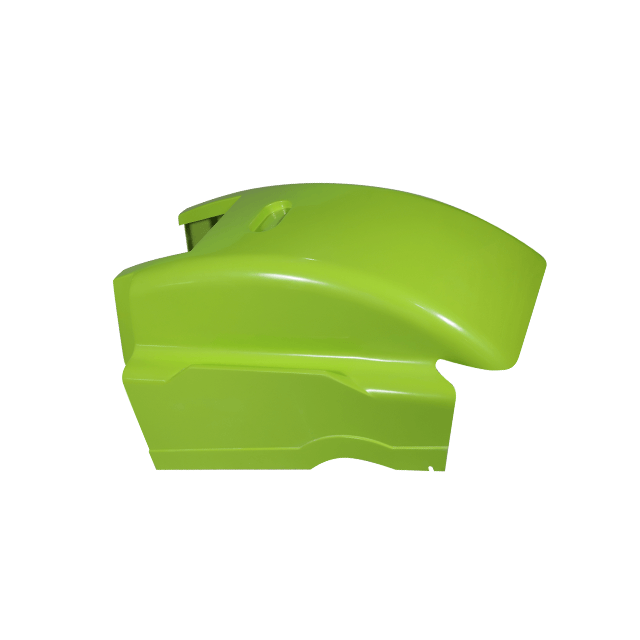
Protecting complex composite geometries requires a multi-layered approach. You cannot rely on a single material to prevent all transit damage. Instead, engineers combine several targeted solutions.
| Protection Solution | Primary Function | Best Use Case | Material Example |
|---|---|---|---|
| Surface Masking | Prevents cosmetic scratches | Class-A automotive panels | Low-tack LDPE film |
| Edge Protectors | Absorbs impact on flanges | Complex geometric borders | Routed EVA foam |
| Custom Dunnage | Prevents part collision | High-volume bulk shipping | Thermoformed plastic trays |
| Rigid Containers | Defends against crush loads | Heavy LTL freight transit | Welded steel racks |
Packaging design must flow directly from part engineering. You cannot select packaging materials blindly. Complex curvatures and draft angles dictate your internal blocking requirements. A part featuring negative draft angles requires flexible dunnage. This allows workers to insert and remove the part without stressing the edges.
You must constantly balance weight against rigidity. We evaluate the inherent stiffness of the fiberglass rtm component itself. Highly rigid parts can snap if the packaging flexes too much during transit vibrations. We rely on ISTA (International Safe Transit Association) testing standards. ISTA 3A vibration tests help determine the exact foam density required to dampen resonance frequencies.
Environmental factors pose another significant threat. Prolonged overseas shipping exposes composite parts to extreme temperature shifts. High humidity inside shipping containers accelerates condensation. This moisture can penetrate unsealed composite edges. We mitigate this by using specialized barrier bags. We also place calculated volumes of desiccant packs inside the crates. This controls internal humidity perfectly.
Compliance and logistics dictate your final crate design. Export shipments demand strict adherence to ISPM 15 standards. This requires heat-treating all wooden packaging materials. Furthermore, you must optimize your pallet footprint. LTL (Less Than Truckload) shipping penalizes oversized crates heavily. FTL (Full Truckload) shipping requires stackable designs to maximize trailer utilization.
| Transit Hazard | Engineering Implication | Recommended Packaging Countermeasure |
|---|---|---|
| Vibration Frequency | Resin matrix micro-cracking | Suspension dunnage (Polyurethane FIP) |
| Thermal Expansion | Warping of tight-tolerance parts | Climate-controlled barrier bagging |
| Forklift Handling | Punctures and crush damage | Reinforced skid bases (ISPM 15 Wood) |
Your manufacturing partner's responsibility does not end at the press. You must vet their post-production handling processes rigorously. Look for automated unloading systems. Manual handling of large composite panels introduces high defect rates. Additionally, inspect their packaging environments. High-quality suppliers pack Class-A parts inside cleanroom environments. This prevents abrasive dust from trapping under protective films.
Demand absolute cost transparency during the quoting phase. Suppliers often obscure packaging expenses. Differentiate between standard expendable packaging costs and custom returnable dunnage. Expendable costs embed directly into the piece price. Returnable racks require an upfront capital expenditure. However, you can amortize these costs over the project's lifetime.
Liability and Quality Assurance protocols require strict definition. Establish clear handover protocols at the shipping dock. You must define who bears the cost of damaged parts. Distinguish clearly between transit vibration damage and inherent manufacturing defects. Implementing a joint inspection SOP (Standard Operating Procedure) prevents painful disputes later.
Apply rigorous shortlisting logic when selecting a vendor. Do not accept a simple piece-price quote. Require all prospective vendors to submit a detailed "Packaging and Dunnage Proposal." This document must accompany their tooling quotes. It should detail pallet dimensions, foam densities, and expected pack-outs per container.
Designing custom packaging carries hidden risks. The dimensional weight penalty remains the most common trap. You might design custom packaging that protects the part flawlessly. However, if it uses excessive volume, freight carriers will apply severe surcharges. Carriers calculate shipping costs based on volume, not just actual weight. You must engineer dunnage that protects the part tightly.
Returnable packaging logistics present another challenge. A closed-loop reusable racking system sounds efficient. Yet, it hides significant administrative costs. You must track the empty racks. You must pay freight to return them to the molding facility. If supply chains stretch across oceans, returnable racks rarely make financial sense.
Sustainability pressures continue to reshape packaging requirements. Regulatory bodies restrict non-recyclable spray foams increasingly. You should transition toward molded fiber packaging where feasible. Readily recyclable mono-materials offer excellent protection. They also help your company meet its ESG (Environmental, Social, and Governance) targets.
Take immediate action to secure your supply chain. First, audit your current composite scrap rates. Identify damage patterns related to transit. Next, request a packaging redesign pilot for your highest-damage SKUs. Finally, establish standardized packaging SOPs with your vendor. Document every material requirement meticulously.
A: RTM Lite parts often have slightly different thickness tolerances. They potentially feature one less-finished side. This simplifies nesting processes significantly. However, they still require robust edge protection to prevent chipping. Standard RTM typically demands comprehensive two-sided surface protection.
A: Molded fiber performs excellently for localized corner protection. It also protects smaller, fragile RTM parts well. However, oversized or extremely heavy panels require more rigidity. You typically need structural wood or steel support to bear the primary load weight.
A: Apply direct surface masking film first. Next, utilize suspended foam dunnage to prevent internal rubbing. Finally, enclose the part in a rigid, fully boxed outer crate. This combination defends against both abrasion and unpredictable forklift impacts.
